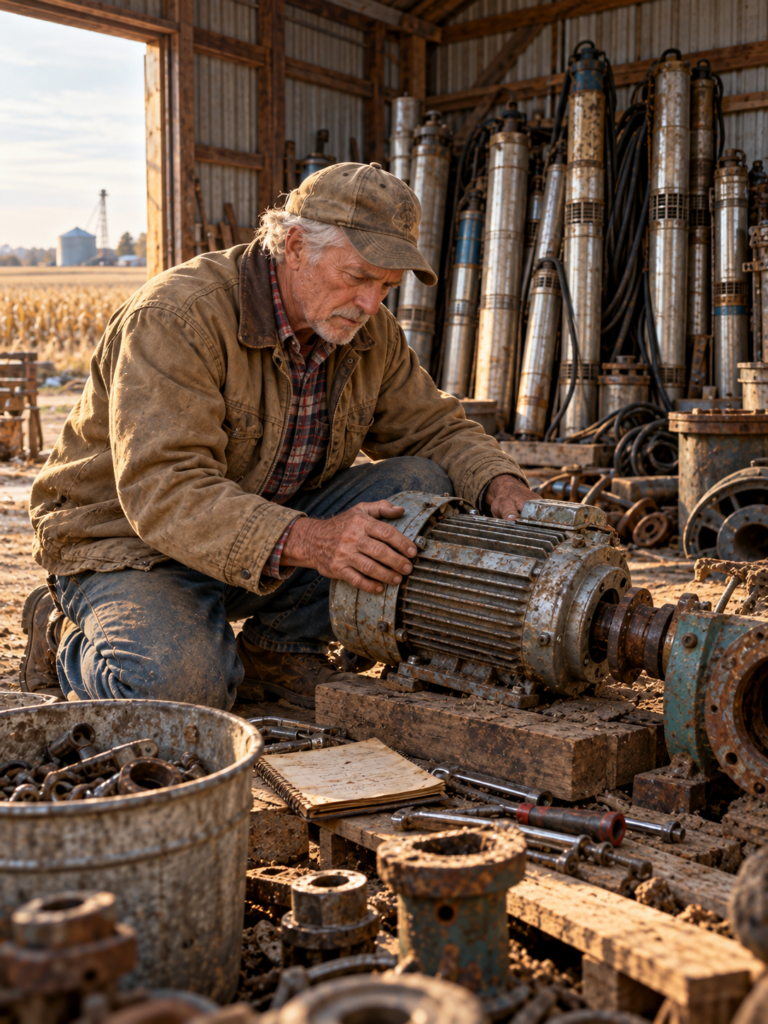
The micrometer closed gently around the shaft surface as Dale adjusted it to the proper contact pressure.
He read the measurement, opened the tool, and took it again.
The numbers agreed.
The wear was not enough to condemn the shaft.
He entered the measurement beside the motor’s identification number, then inspected the bearing seat.
That was the second encouraging result.
A pump that had been discarded as a complete assembly still contained components that could be returned to service.
But Dale did not confuse a promising inspection with proof that his idea would work.
There were forty more pump units to examine.
And even if enough motors survived, connecting them to a different hydraulic assembly presented another problem.
The original Grundfos components were designed to work together.
The Goulds turbine bowls he wanted to use belonged to another design.
Their shafts could not simply be bolted together.
Dale spent the following weeks separating everything into groups.
Twenty-three of the original forty-one motors were too damaged for economical rebuilding.
Burned windings.
Corroded rotors.
Cracked housings.
Water-damaged internal components.
He did not attempt to rescue them for sentimental reasons.
He kept useful material and set aside what could not reasonably be restored.
The other eighteen motors became the focus of his project.
Their frames were intact, and their remaining defects were problems he could measure and address.
The pump bowls also contained recoverable components, although many of their impellers were badly worn.
At the end of each workday, Dale cleaned the bench and entered his findings into the binder.
He was building a record before he was building a pump.
Eventually, he telephoned Pete Schreiber, the Goulds distributor in Omaha who had supplied parts to him for years.
Dale described the motors.
Then he explained the different bowl assemblies he hoped to install.
Pete listened.
He did not laugh.
He thought the proposed mechanical connection was possible, provided the coupling and operating requirements were correct.
But Goulds did not manufacture that combination.
There would be no official documentation certifying it as a complete Goulds product.
Dale understood the distinction.
He was proposing a custom machine and would have to establish its performance himself.
He ordered eighteen turbine bowl assemblies.
Then he sat at his workbench with graph paper and began drawing an adapter coupling.
The dimensions had to be precise.
The coupling needed to connect the two shaft designs without introducing damaging misalignment.
A poorly made connection could destroy a perfectly good motor.
Dale measured carefully, noted the tolerances, and prepared a dimensioned drawing.
He took it to Gary Hendrix, who operated a precision machine shop in Council Bluffs.
Gary examined the drawing and agreed to manufacture the parts.
Two weeks later, Dale had the couplings.
He assembled the first hybrid pump during the winter of 1993.
Before he installed it in a well, he built a test arrangement using a fifty-gallon stock tank and a recirculating loop.
He added sand to the water to approximate the abrasive conditions he had measured in his aquifer.
Then he switched on the pump.
Water began circulating.
The motor ran.
But one hour of operation would prove very little.
So Dale left the system running under observation.
He monitored its behavior and recorded the test conditions.
After seventy-two hours, he shut it down.
He removed the pump from the test arrangement and disassembled the hydraulic assembly.
The question was no longer whether the motor could turn the impeller.
The question was whether the impeller and wear surfaces could tolerate the sand.
He cleaned the parts and placed them on the bench.
Then he checked their clearances against the measurements recorded before the test.
The difference was within two thousandths of an inch.
It was encouraging.
He ran another seventy-two-hour test.
The measurements remained similarly stable.
Dale placed the results in the binder.
The original distributor had classified the failed pumps as uneconomical to rebuild in their existing configuration.
But Dale’s first completed hybrid had passed a controlled test that directly addressed the problem he had identified.
He telephoned Pete in Omaha and read him the results.
Pete recognized their significance.
Still, one successful test did not establish the service life of every future unit.
Dale knew that.
He returned the first pump to the bench, opened the next tagged motor, and began preparing the second rebuild.
The second motor lay open beside the first set of completed test records.
Dale checked its bearing surfaces, compared the readings with his notes, and began preparing the replacement components.
He worked through the winter.
There was no deadline imposed by a customer.
No sales contract.
No pressure from a distributor.
His primary business was still farming.
The pump project occupied the cold months, when the fields were frozen and the agricultural work slowed enough to leave time for careful repairs.
He did not rush the process.
By the end of the first winter, he had learned which measurements mattered most during assembly and which components needed particular attention.
Each subsequent rebuild became a little more predictable.
He cleaned housings, installed replacement seals, checked alignment, and assembled the turbine bowls using his machined adapters.
Then he tested the completed units.
The same procedure.
The same measurements.
The same entries in the binder.
He was not trying to make eighteen pumps look new.
He wanted eighteen machines whose condition he could describe accurately.
By 1996, eighteen complete hybrid units stood on wooden pallets inside the shed.
Dale had invested approximately $14,000 in parts, machining, and materials.
The cost of buying eighteen comparable new Grundfos units would have been approximately $63,000.
That difference mattered.
But the financial arithmetic was only part of what he had learned.
He had confirmed that the discarded equipment contained substantial recoverable value, provided the components were selected correctly and rebuilt for conditions they could reasonably tolerate.
The original pumps had not failed because every part was inherently worthless.
They had been operating in water conditions that accelerated wear in their original hydraulic design.
Changing the bowl assembly addressed the mismatch Dale believed was responsible for much of that deterioration.
He kept the completed units stored under cover.
Each one carried a tag.
The binders contained its measurements and test history.
And Dale went back to farming.
He did not call Ronnie Fitch to announce what he had accomplished.
Ronnie continued operating Heartland Ag Supply.
The dealership still sold and serviced irrigation equipment throughout the county.
Customers continued to experience pump failures.
The normal process involved pulling the failed unit, arranging the warranty replacement when eligible, installing the replacement, and charging for the service involved.
It was a familiar business model.
But the economics began changing in 2001.
Heartland’s distributor was acquired by a larger regional company.
The new warranty terms reduced the coverage window from two years to eighteen months.
They also required documented water-quality testing before certain warranty claims would be approved.
Ronnie had not made such testing a standard part of his installation process.
When his first claim was denied for lack of documentation, he argued with the distributor.
The decision stood.
He absorbed the replacement cost.
Several additional claims created the same problem.
Eventually, Heartland changed its sales procedures to include water testing, adding expense to new installations.
Customers noticed the higher bills.
The dealership’s margins tightened.
Service work continued, but warranty reimbursements no longer supported the operation as they once had.
Two employees left in 2002 and were not replaced.
The business remained prominent, but it was no longer operating with the strength it had enjoyed a decade earlier.
During those years, Dale’s rebuilt pumps remained in his shed.
He had already spent the money required to build them.
They were not tied to a dealership inventory account or a financing agreement.
They were available when someone had a suitable use for them.
That opportunity arrived in October 2002.
Ken Albrecht farmed 480 acres about two miles north of Dale.
His irrigation pump had failed again.
It was a four-year-old Grundfos unit that Heartland had already pulled multiple times.
The service technician determined that the motor was burned and the bowl assembly badly worn.
A new installed pump was quoted at $2,100.
Ken knew Dale had been working with discarded pumps.
That evening, he telephoned.
“Do you still have those rebuilt units?”
Dale said he did.
Ken drove over the next morning.
Dale opened the shed and led him to a pump whose specifications matched the requirements of Ken’s well.
He explained the hybrid construction.
Then he showed Ken the test results.
The seventy-two-hour runs.
The clearance measurements.
The assembly records.
Ken examined the binder.
He had known Dale for years, but knowing a man was careful was not the same as understanding how much care had gone into the equipment.
Dale told him the installed price would be $800.
He also offered to replace the unit from his remaining inventory if it failed within two years.
Ken agreed.
On a Wednesday in October, Dale installed the hybrid in Ken’s well.
He checked the electrical load, discharge pressure, and water flow.
The pump performed close to the required specification.
Dale entered the installation date and measurements into the binder.
Then he returned home.
The pump kept running.
As the months passed, other farmers began asking questions.
They had heard that Dale was installing rebuilt pumps assembled from components originally discarded by Heartland.
Some were skeptical.
Others were interested because they had experienced repeated failures or were facing expensive replacement quotes.
Dale did not offer a universal solution.
He matched available units to suitable wells.
He showed customers what he had measured.
He explained what he had changed.
By spring 2003, seven neighboring farmers had received rebuilt units.
By autumn, the number had reached eleven.
There had been no reported failures among those installations.
That was more persuasive to neighboring farmers than any advertisement.
It also reached Ronnie Fitch.
One November afternoon, Ronnie drove to the Musselman farm without calling ahead.
Dale was leaving his machine shop with grease on his hands.
Ronnie stood beside his truck.
He had heard Dale was selling pumps.
Dale explained that he was supplying and installing rebuilt units for neighboring farmers rather than operating a conventional dealership.
Ronnie questioned the distinction.
Dale did not argue at length.
The pumps were working.
He was maintaining installation records.
And he had discussed the associated liability questions with his insurance agent and attorney.
Ronnie looked toward the shed.
He asked to see the machines.
Dale opened the door.
The interior no longer resembled the disordered pile behind Heartland Ag Supply.
The rebuilt pumps stood on pallets.
Each carried an identification tag.
The binders were stored above them.
Ronnie walked slowly down the row.
He picked up a binder.
There were assembly measurements, test results, and records of completed installations.
He examined an adapter coupling visible on one of the units.
This was not the collection of broken machines he remembered giving away.
It was a documented rebuilding project involving specialized parts and years of careful testing.
Ronnie asked how many pumps Dale had installed.
Eleven.
He asked about failures.
None reported.
Ronnie set the binder back on its shelf.
He reminded Dale that he had called the old pumps scrap.
Dale agreed.
There was no need to deny the conversation.
Ronnie had classified the failed assemblies according to the economic and warranty practices of his dealership.
Dale had examined them as individual collections of reusable and unusable components.
Their conclusions had been different because they were answering different questions.
Ronnie wanted to know whether the original pump assemblies were worth repairing through his established service process.
Dale wanted to know whether selected parts could become reliable equipment in another configuration.
The results now stood between them on wooden pallets.
Ronnie left without making an offer.
Outside, he sat in his truck for a short time.
Then he lowered the window and raised the question of liability exposure.
Dale answered that he had sought professional advice and understood the responsibilities he had accepted.
Ronnie drove away.
The following years did not improve Heartland’s position.
Warranty economics remained difficult.
The dealership lost major service contracts to a competitor based in Council Bluffs.
Its employee count continued falling.
By the end of 2006, a building designed for twelve employees housed an operation employing only four.
In February 2007, Ronnie told the remaining staff that Heartland Ag Supply would close.
He arranged continued pay through the end of March, sold the property and remaining inventory, and retired to Avoca.
The closing was not caused by one farmer’s workshop.
It followed years of changing distribution terms, declining margins, staffing losses, and competition.
But the contrast remained striking.
The dealership that had discarded the pumps was gone.
And the machines Dale had rebuilt were still supplying water.
By then, Dale was eighty-one.
He had installed twenty-two rebuilt units for neighboring farmers through the years of the project, without a reported failure among those installations.
Seven prepared units remained in his shed.
His son Gary had been helping with the farming operation since 1998 and knew the rebuilding process intimately.
Gary understood the test records.
He knew which parts had been replaced.
He knew how the adapter couplings had been made.
And when his father’s health began declining in 2009, Gary gradually assumed more responsibility for the farm and its equipment.
The shed passed into his care along with the rest of the operation.
One winter morning, Gary opened the door and examined the seven remaining units.
Their tags were still attached.
Their binders were still on the shelf.
But years in storage could affect seals and other components, even when the original rebuild had been sound.
Gary brought the first pump to the bench.
He disassembled it.
He inspected the motor and hydraulic components.
He replaced materials that had deteriorated during storage.
Then he recorded the new measurements on a fresh page.
He worked through the remaining units in the same way.
He was not merely inheriting a collection of old machines.
He was taking responsibility for the accuracy of the records attached to them.
In April 2011, another farmer arrived.
Daryl Opp had received a $2,400 quote for a replacement irrigation pump.
He had heard about Dale’s rebuilt units from Ken Albrecht.
Gary showed him the shed and the test binders.
Then he brought out the original adapter drawing.
It was the same graph-paper design Dale had prepared in the winter of 1992–1993.
Daryl examined the dimensions and asked whether Dale had made the drawing himself.
Gary said yes.
Then Daryl asked how old Dale had been.
Gary answered that his father had been sixty-seven.
The same age Daryl was then.
Daryl agreed to purchase a rebuilt pump for $800 installed.
Gary completed the installation that April and entered its performance measurements into the binder.
The pump operated successfully.
But the drawing in Daryl’s hands represented something larger than one economical replacement.
An idea Dale had developed late in life was now being used by the next generation.
And the old documents were about to become more important than Gary had expected.
Gary returned the graph-paper drawing to its protective folder after Daryl Opp’s pump was installed.
The paper had begun to soften at the folds.
Its pencil lines were still clear, but the edges showed the wear of repeated handling.
It was not a factory blueprint.
There was no manufacturer’s approval stamp.
It was his father’s drawing, made at a farmhouse workbench with measurements taken from two different pump designs.
Gary understood every dimension.
He also understood why his father had kept the original rather than replacing it with a cleaner copy.
The drawing recorded the reasoning behind the part.
Without it, another mechanic might see an unusual coupling and assume it was a crude improvisation.
With it, the relationship between the components could be measured, checked, and reproduced.
Dale had not expected the drawing to become a family heirloom.
He had made it because there was a mechanical problem that needed an accurate solution.
That distinction was important to Gary.
The family had never treated old equipment as valuable simply because it was old.
A machine had to justify its place.
The same principle applied to the records.
They were useful because they described real conditions, measured at real times, by people who had actually inspected the equipment.
In the months following Daryl’s installation, Gary continued reviewing the pump binders.
He found himself returning frequently to the earliest records.
The first Goulds turbine pump his father purchased in 1962.
The original service measurements.
The maintenance performed on the other three wells as Dale expanded his irrigation system.
The water-quality result from 1984.
And the rebuilding project that began after Ronnie Fitch laughed at the idea of salvaging his dealership’s discarded equipment.
Gary remembered parts of that period.
He had helped with the rebuilds and knew how methodically his father had worked.
But reading the older entries revealed the full sequence in a way memory could not.
A measurement recorded before an assembly test.
A small change made to the next coupling.
A note about sealing.
A later measurement confirming that a revised component was behaving as intended.
Dale had not begun with the finished answer.
He had worked toward it through inspection and testing.
That was why the binders mattered.
They preserved the unsuccessful possibilities as well as the successful ones.
In October 2012, Dale made one of his final entries in his personal pump service records.
His number-three well pump was due for scheduled maintenance.
He removed it, inspected the impellers, replaced the shaft seal, and checked the bearing clearances.
Then he compared the measurements with those taken at its previous service in 2007.
The clearances remained within two thousandths of an inch of the earlier readings.
He entered the figures carefully.
At the bottom of the page, he added a brief observation.
“Design holding up well.”
That was all.
No claim of genius.
No mention of Heartland Ag Supply.
No reflection on the years Ronnie had dismissed his idea.
Just a conclusion supported by the numbers above it.
Dale died in March 2013 at the age of eighty-seven.
He had worked the family’s farm for more than half a century.
The four irrigation wells he had maintained had supplied the operation across decades of changing weather, crops, and equipment.
His original Goulds pumps and later hybrid rebuilds had served him without recorded in-service failures.
His funeral was held at First Lutheran Church in Carson.
About two hundred people attended.
Ken Albrecht was there.
So was Daryl Opp.
Other farmers who had received rebuilt pumps came to pay their respects.
Gary sat in the front pew with his wife and two children.
Leah, twenty-two, was studying agricultural engineering at Iowa State University.
Marcus, nineteen, had been helping on the farm for years.
Ronnie Fitch attended as well.
He sat near the back.
By then, Heartland Ag Supply had been closed for six years.
The old dealership no longer occupied the position it had held when nearly every farmer in the area purchased the same type of pump through the same supplier.
Ronnie had retired to Avoca.
He had a garden.
And he had not returned to the Musselman farm since the afternoon in 2003 when he had examined the rebuilt units.
After the funeral service, photographs of Dale were arranged near the reception room entrance.
There was a picture of him working with his father Harold.
Another showed him on a tractor in the early 1970s.
One photograph showed Dale standing inside the shed with a pump component in his hands.
The wooden pallets and service binders were visible behind him.
Ronnie stood before that photograph for a long time.
Gary noticed him.
He did not approach.
There was nothing that needed to be settled at a funeral.
Ronnie had once dismissed a rebuilding idea that later proved useful.
Dale had never needed an apology to keep working.
His results existed independently of Ronnie’s opinion.
Eventually, Ronnie set down his coffee and left.
Gary watched him go.
Then he turned back toward the people who had come to remember his father.
The photograph stayed on the table until the reception ended.
Afterward, it returned to the machine shop, where the family could see it during ordinary working days.
The farm continued.
Gary took primary responsibility for its operation.
The wells still needed servicing.
The fields still needed irrigation.
Old seals still wore out.
And new equipment introduced new problems that no amount of experience could entirely prevent.
Leah graduated from Iowa State University in 2014 with a degree in agricultural engineering.
She returned to work alongside her father.
She had grown up with the pump binders.
As a child, she knew they were important because her grandfather handled them carefully and because nobody was allowed to replace a part without recording what had been found.
At university, she learned to connect that practical habit with formal engineering analysis.
Fluid mechanics.
Electrical drives.
Hydraulic systems.
Soil properties.
Measurement and control.
She returned to Carson with a deeper understanding of the equipment her grandfather had maintained and questions about how the farm might operate more efficiently.
The hybrid pumps had solved one significant problem.
Their turbine bowl assemblies were better suited to the sandy local groundwater than the original hydraulic assemblies.
But they still operated using traditional fixed-speed arrangements.
Their output did not automatically adjust to changing field moisture conditions.
Leah began studying how variable-frequency drives could be used to control pump speed.
She read technical papers and examined agricultural field trials.
She compared the findings with the operating characteristics and electrical requirements of the remaining hybrid units.
By spring 2019, she was ready to propose a project.
Gary was at the kitchen table when she brought out the calculations.
She placed a printed study beside a yellow legal pad.
Then she explained her plan.
The remaining five hybrid pumps would be converted to variable-frequency-drive control.
Soil-moisture sensors could provide information about irrigation demand.
The controllers could then adjust pump operation rather than requiring each unit to run continuously at one fixed speed and flow rate.
Gary examined her calculations.
The controller hardware would cost approximately $1,200 per unit.
Based on the field-trial data Leah had reviewed, she estimated potential energy savings between thirty and forty percent.
The projected payback period was approximately 2.8 years per well.
Those were estimates, not guarantees.
Actual savings would depend on how the equipment performed under their field conditions.
Gary turned the printed study over.
Then he examined the numbers again.
He recognized the process.
His father had once compared water-quality measurements with pump design requirements and concluded that the standard equipment configuration was not ideal for their wells.
Now Leah was comparing operating data with modern control methods and asking whether another change could improve performance.
Gary said his father would have appreciated the approach.
Leah agreed.
The family approved the work on all five units.
She installed the controllers and soil-moisture sensing system, with the necessary adjustments for the equipment’s electrical and hydraulic requirements.
The project did not replace Dale’s entire pump design.
It added control capability to machines that had already demonstrated years of useful service.
Leah documented the installations.
She recorded the baseline electrical consumption, controller settings, and observed performance.
Then she began comparing the results.
The completed system reduced energy use by approximately thirty-four percent relative to the previous operating baseline.
That was close to the range she had estimated.
It also meant that the old hybrid equipment could continue serving the farm under a more responsive irrigation arrangement.
The machines now contained components originating from several very different periods.
Grundfos motors recovered from failed pump assemblies.
Goulds turbine bowls selected for their suitability to local groundwater.
Custom adapter couplings designed on graph paper in the early 1990s.
And modern variable-frequency-drive controllers informed by sensor measurements.
No single manufacturer had created the complete arrangement.
Its evolution had occurred through repeated decisions about what the equipment actually needed.
Leah began keeping digital maintenance records alongside the original binders.
She entered the pump identifications, service dates, operating data, and measurements so that the information could be searched more easily.
Gary kept the paper records.
The old binders remained on the shelf above the bench.
They were brown, with red stripes along the spines.
Electrical tape reinforced several cracked hinges.
Some had been in use since the early 1960s.
The paper was stained in places.
A few pages carried fingerprints left by hands that had been handling grease or sealing compound.
But the measurements were still readable.
The records described equipment spanning three generations.
Harold Musselman had purchased the family land in 1948.
He had installed the first well on the property in 1951, giving the farmhouse running water.
Dale, still a child, had helped by handing tools to his father as the work progressed.
That early experience had shaped how he thought about water.
It was not enough to assume a well would produce what the farm needed.
Someone had to understand the ground, the equipment, and the maintenance required.
Years later, Dale applied the same approach to his Goulds pumps.
He did not wait for complete failure before investigating wear.
He measured components during scheduled maintenance.
He recorded what changed.
He learned which signs were ordinary and which suggested a developing problem.
When he began examining the failed Grundfos pumps, he already possessed decades of relevant experience.
That was what Ronnie Fitch had underestimated.
Ronnie’s dealership experience was genuine.
He knew how to sell equipment, arrange warranty service, and manage a large customer base.
His judgment that the failed pumps were not economical to rebuild through the normal dealership process was understandable within that business model.
But Dale was evaluating a different possibility.
He did not need to restore every pump to its factory configuration.
He needed to identify parts that could still perform useful work and design a system suitable for the water he actually had.
The distinction was small enough to be overlooked.
Its consequences lasted decades.
The distributor’s rejection of a complete assembly did not establish that every motor, housing, shaft, or bowl component had no remaining use.
Dale had proved that by inspection.
Then by rebuilding.
Then by testing.
And finally through years of operation in actual wells.
He also recognized that salvage required judgment.
More than half of the original forty-one motors were too badly damaged for economical rebuilding.
He had not attempted to save them all.
The successful project depended partly on his willingness to reject unsuitable components.
Careful reuse was not the same as refusing to discard anything.
That principle survived in Gary’s maintenance work and Leah’s later engineering decisions.
The family did not preserve equipment merely to honor Dale.
They preserved equipment that could still be made useful, documented its limitations, and improved it where the evidence supported improvement.
Across Pottawattamie County, the pumps Dale had installed for neighboring farmers acquired histories of their own.
Ken Albrecht’s installation continued supplying water.
Daryl Opp’s pump remained in service.
Other farmers retained machines assembled from motors that had once been regarded as unsalvageable.
According to the family’s later account, eleven of the twenty-two neighborhood installations were still operating after many years of use.
Meanwhile, the five hybrid units Leah had modernized remained part of the Musselman farm’s irrigation system.
Their performance was monitored.
Their service information was recorded.
And the old drawings were preserved beside newer technical documentation.
Ronnie Fitch was no longer involved in the work.
His dealership had closed long before the variable-frequency-drive project began.
Nothing in the later improvements required his endorsement.
Gary did not hold the original disagreement against him.
As far as he knew, Dale had never treated Ronnie as an enemy either.
They had reached different conclusions about the value of the same discarded equipment.
One had ended the matter with a laugh.
The other had gone home, opened a notebook, and started measuring.
That was the difference that lasted.
One morning, Gary entered the machine shop and passed the photograph his mother Eleanor had taken in 1995.
She had died in 2004, but the picture remained where she had hung it.
Dale stood in the shed, holding an adapter coupling toward the light.
He wore a canvas jacket and a seed cap.
His hands were dark with grease.
He was not looking at the camera.
He was looking at the component.
The photograph captured him in the middle of an inspection.
A small part held between his fingers.
A question being answered through measurement rather than assumption.
Gary stopped before the picture.
He remembered watching his father work.
The slow adjustments.
The second measurements.
The way he would put a part down and return to the drawing when something did not fit.
It had seemed excessively careful when Gary was younger.
Now he understood that the care was what allowed old equipment to become dependable.
He turned toward the workbench.
One of the service binders lay open.
Leah had entered newer performance data alongside the earlier records.
Her figures were different from Dale’s.
They described electrical consumption and changing pump speed rather than only impeller clearances and shaft bearings.
But the underlying question had not changed.
Was the equipment doing what the operator believed it was doing?
And what evidence supported that belief?
Gary closed the binder and returned it to the shelf.
The photograph remained above the bench.
Outside, the irrigation system was operating.
The pumps were moving water from the same sandy aquifer that had caused so much trouble for the original equipment.
The groundwater had not changed to accommodate the machines.
The machines had been adapted to accommodate the groundwater.
That was the truth behind the shed full of discarded pumps.
Not that every failed machine could be saved.
Not that manufacturers knew nothing.
Not that an experienced dealer had been wrong about every aspect of his business.
The evidence supported something more precise.
A machine could be uneconomical to repair in its original configuration while still containing components suitable for another carefully engineered application.
Dale had recognized that possibility.
He had tested it.
And instead of treating the first successful result as sufficient, he spent years confirming the work.
The business that had accumulated the failed pumps eventually disappeared.
The farm that rebuilt selected parts continued using them.
And the records passed from father to son to granddaughter.
Gary switched off the shop light as he left.
In the quiet behind him, the binders stood on the shelf, their worn spines facing outward.
The original adapter drawing remained inside its folder.
The photograph stayed on the wall.
And out beyond the buildings, the pumps continued supplying water to the fields.
Forty-one discarded pump assemblies had once arrived on Dale Musselman’s flatbed trailer.
They were not a hidden fortune.
They were a collection of failures that required sorting, measurement, engineering, and years of patient work.
Dale had been sixty-six when he first looked into Ronnie Fitch’s shed.
He had been sixty-seven when he completed the first successful hybrid.
He was old enough that many people would have expected him to stop taking on unfamiliar mechanical problems.
Instead, he began a project whose results outlived him.
The final value of those pumps could not be calculated solely from their original purchase price, their salvage cost, or even the savings they later produced.
Part of their value was the knowledge they carried forward.
Harold had taught Dale to understand the machinery that supplied his land.
Dale had taught Gary to record what he learned.
Gary had preserved that work for Leah.
And Leah had used her engineering education to make the same equipment more efficient.
The pumps that Ronnie had dismissed did not become useful because someone simply believed in them.
They became useful because Dale discovered which parts were sound, proved what could be rebuilt, and refused to confuse a label with a measurement.
Years later, that distinction was still moving water beneath the Iowa fields.
And above the old workbench, Dale’s last service records remained ready for the next person willing to open them.